Sector Expertise
Our pharmaceutical experience spans sterile, non-sterile, high-potency, and inhalation manufacturing environments; the highlighted project below is one representative example of that broader capability.
From concept to commercial readiness: OSD, Injectables, HPAPIs, Ophthalmics, Inhalation Products, and more, guided by proven cGMP and regulatory expertise.
Our pharmaceutical experience spans sterile, non-sterile, high-potency, and inhalation manufacturing environments; the highlighted project below is one representative example of that broader capability.
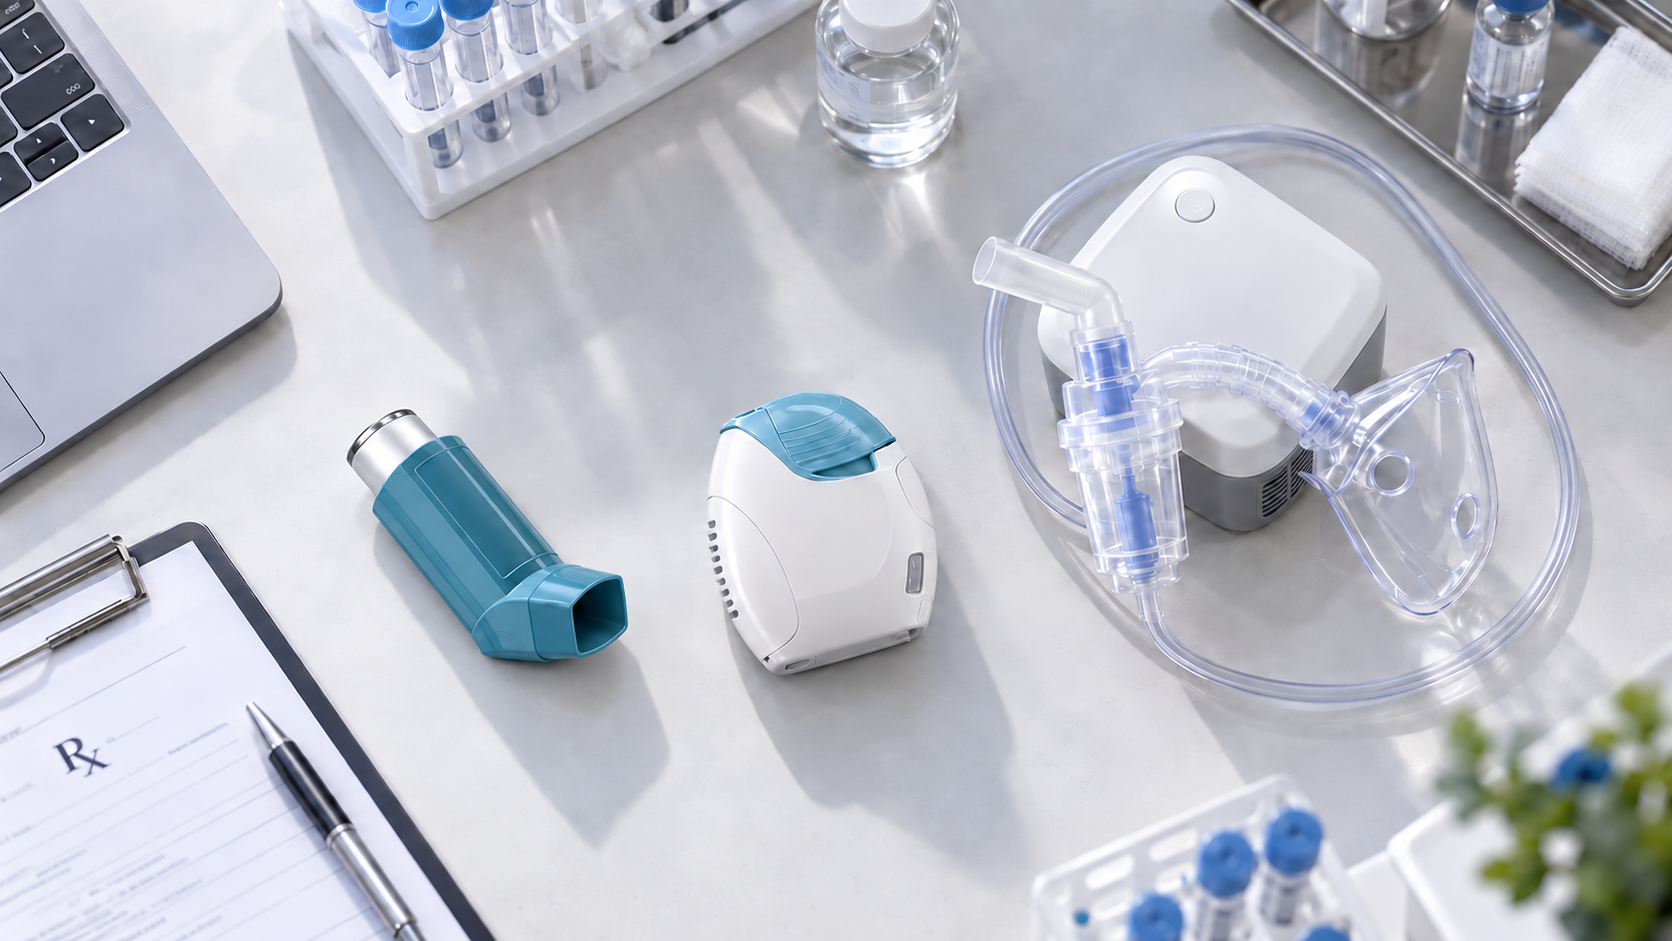
EPC delivery of a 10,000 m² greenfield pharmaceutical manufacturing campus for inhalation therapies based on AstraZeneca technology. The facility included MDI (Metered Dose Inhaler), DPI (Dry Powder Inhaler), and nebulizer product lines; integrated drug-device assembly; HPAPI manufacturing areas; warehousing; R&D and analytical laboratories; administrative facilities; cleanrooms; and complete clean and black utility systems.
The project integrated potent pharmaceutical compounds, complex inhalation formulations, and precision medical device assembly on a single manufacturing platform. Critical requirements included HPAPI containment, cross-contamination prevention, stringent environmental controls, aseptic and non-aseptic processing interfaces, integrated drug-device traceability, and compliance with international pharmaceutical and medical device standards. The facility also required specialized handling of hazardous waste streams and contaminated process effluents while maintaining uninterrupted production and regulatory compliance.
Engineered and constructed a fully integrated manufacturing campus featuring segregated containment zones, advanced cleanroom systems, pressure cascades, HEPA-filtered HVAC, containment isolators, and dedicated HPAPI handling suites. The design incorporated CIP/SIP systems, a Building Management System (BMS), an Environmental Monitoring System (EMS), automated process controls, and specialized waste and effluent treatment systems. Production areas were optimized for MDI, DPI, and nebulizer manufacturing, including drug formulation, device assembly, filling, packaging, and quality control operations. Comprehensive Commissioning, Qualification, and Validation (CQV) activities were performed to support regulatory readiness and operational excellence.
Completed in 2011 as a state-of-the-art inhalation product manufacturing facility, providing end-to-end capabilities for pharmaceutical and combination drug-device products. The facility was completed with full CQV documentation and designed in alignment with EU GMP, WHO GMP, ISPE Good Practice principles, ISO 14644 cleanroom standards, and international regulatory expectations for inhalation and high-potency manufacturing.